Carbon steel fittings in construction of installations
Materials
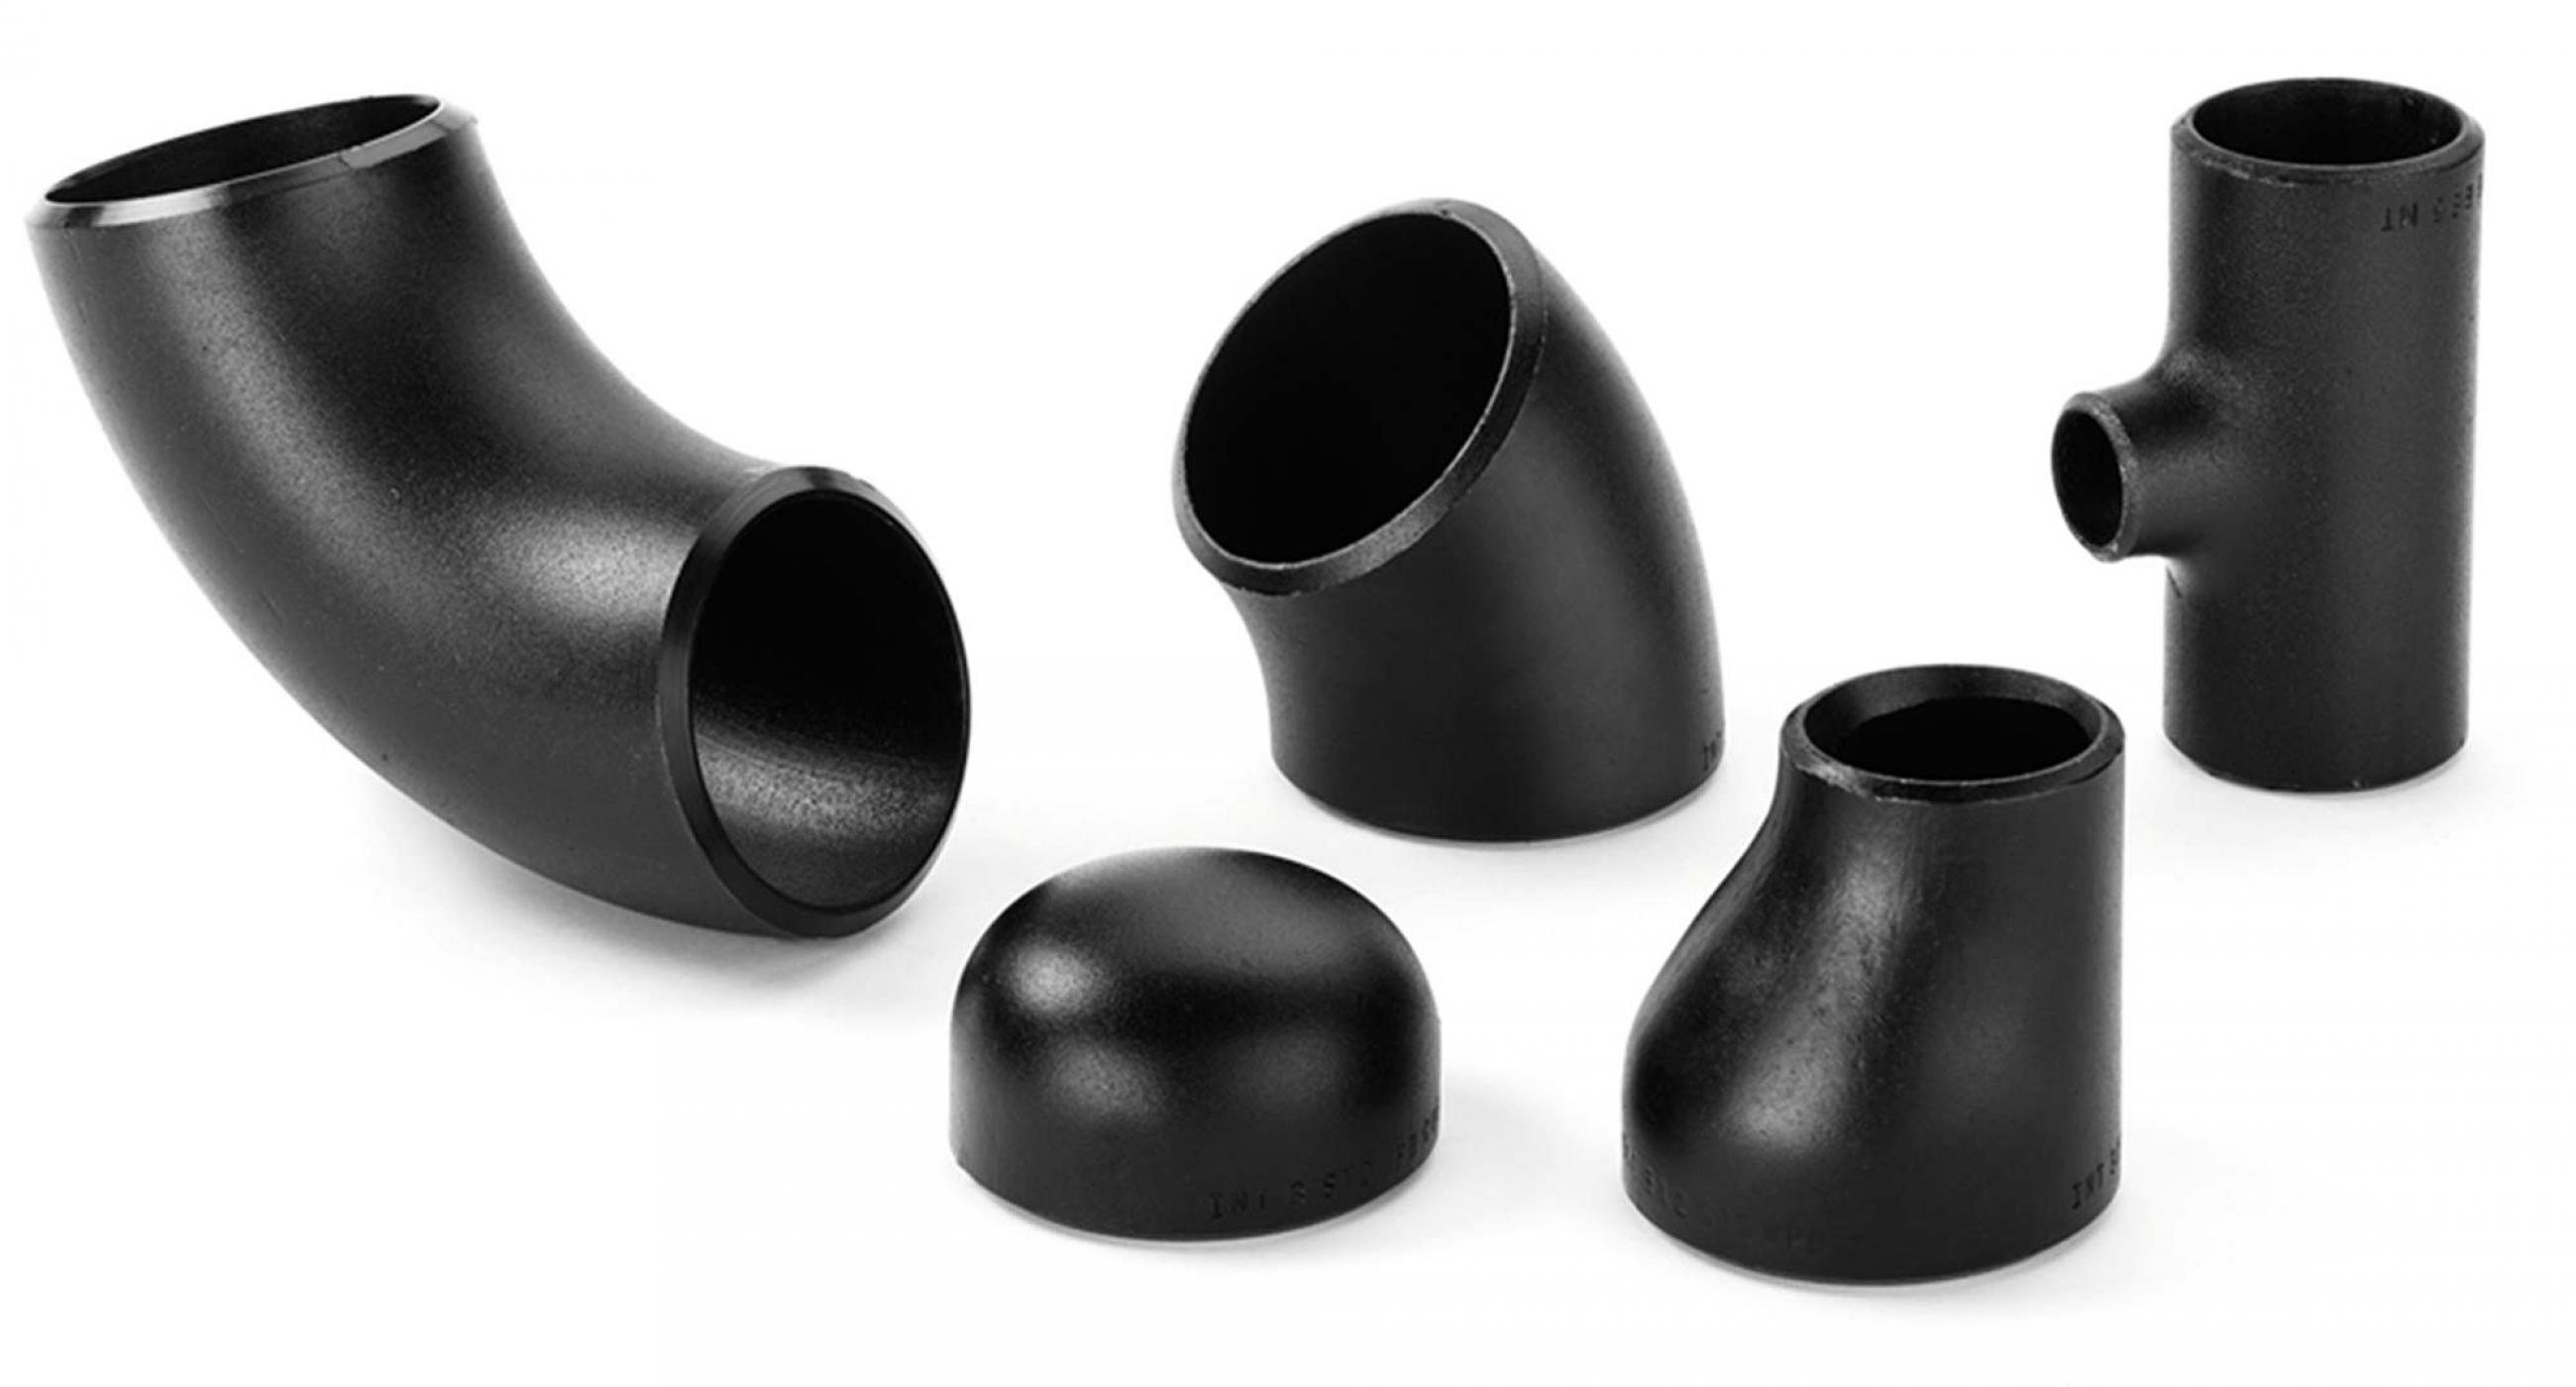
Intertubi manufactures and markets industrial carbon steel fittings. Here are the elements we have in the catalog. Contact us for custom quotes.
21 September 2026
Materials
The construction of industrial plants begins with good system design and, above all, with the selection of components. Today we look at carbon steel pipe fittings, which must meet several key requirements:
Leak-tightness and safety
Performance
Material quality
Versatility of fitting types
Certification
To achieve these goals, the starting point is the appropriate manufacturing technique, selected to obtain the desired final shape while retaining the necessary mechanical properties. This ensures the required performance, together with the selection of the material best suited to operating pressure and temperature.
Versatility also depends on choosing from an adequate range of fitting types, all manufactured and certified according to the relevant standards.
Manufacturing techniques for carbon steel fittings
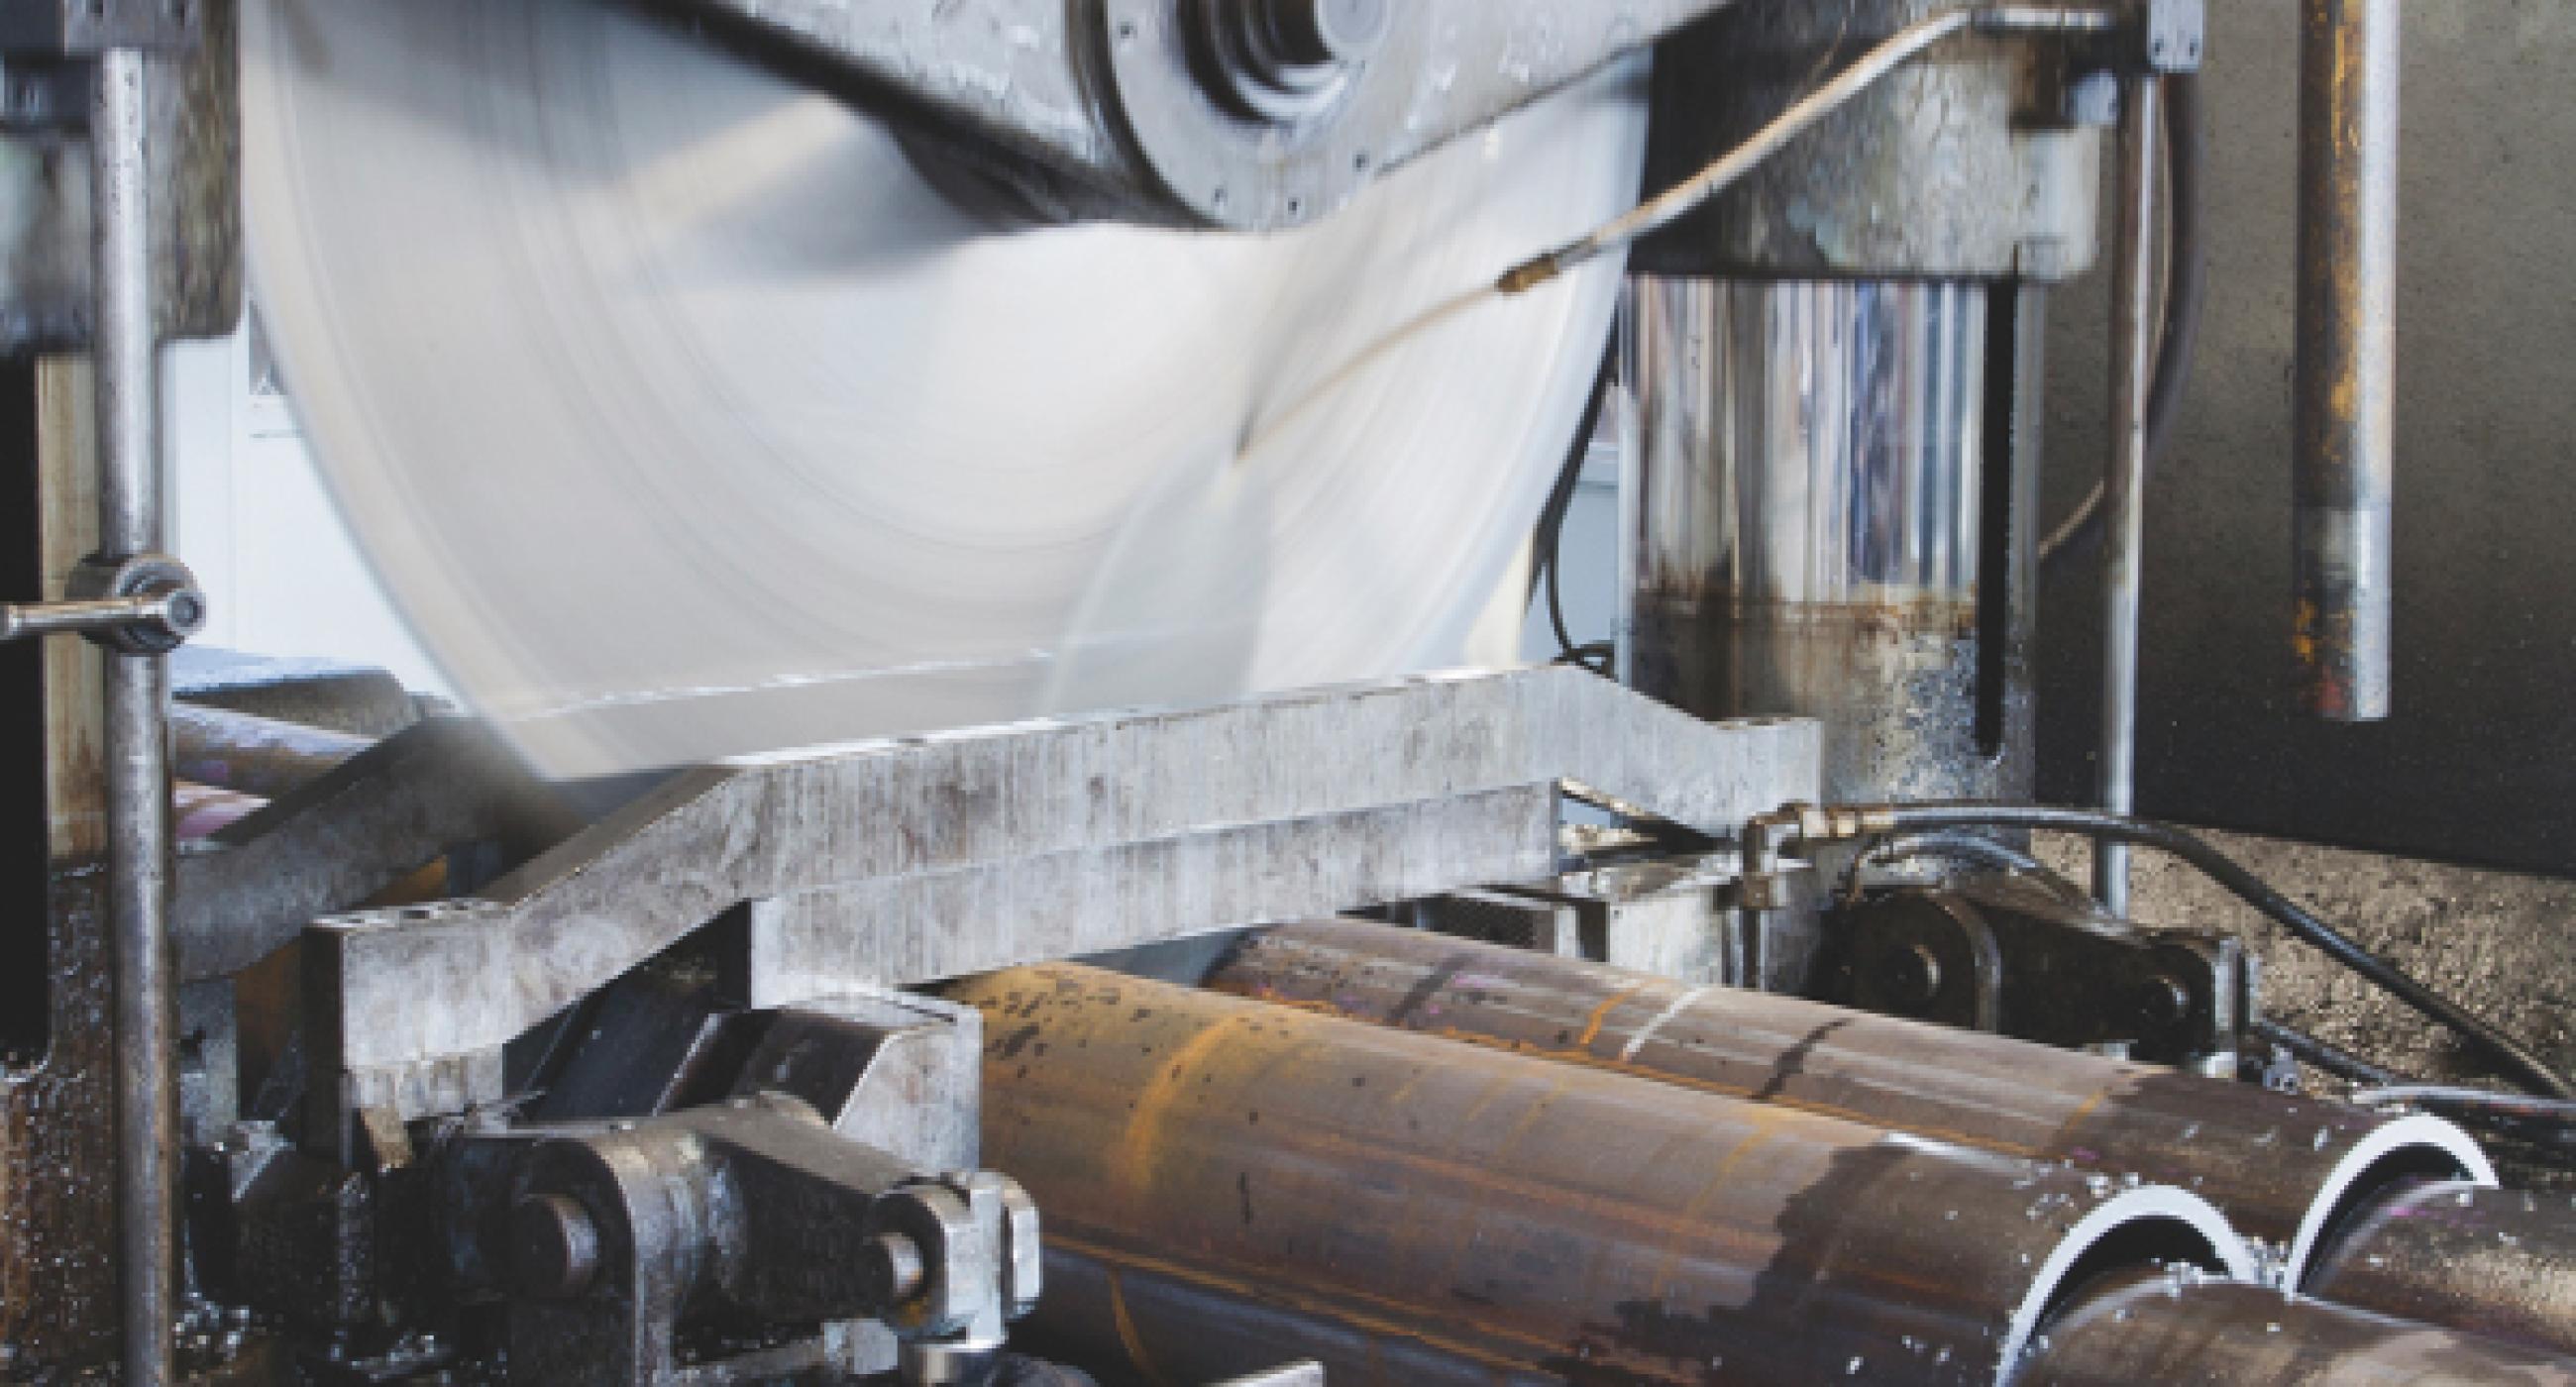
Carbon steel fittings are manufactured from welded steel pipes or steel plates of the required thickness, which are processed differently according to the component being produced.
HYDROFORMING: a process used especially to manufacture equal and reducing tees. The pipe's lateral branch is formed by the action of a pressurised fluid, usually oil.
DEEP DRAWING: a sheet-metal forming process performed with a press, usually cold, designed to give fittings higher resistance to yielding.
FORGING: carried out hot, forging is similar to deep drawing but produces a more ductile finished component. Both techniques are commonly used for open-ended products such as dished ends.
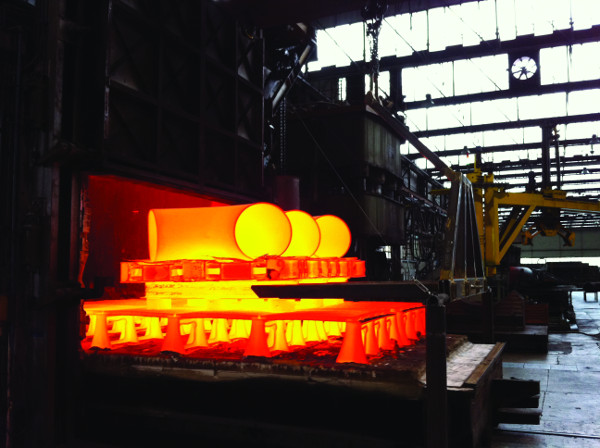
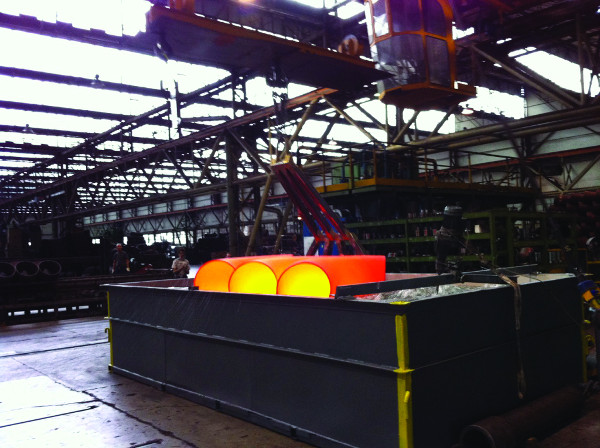
HOT FORMING: after heating the pipe to the temperature most suitable for the process, shaped punches deform the material to produce components such as standard or long-radius elbows. This is one of the most established manufacturing processes. Experience and know-how developed over the years have made it possible to produce components with highly consistent wall thicknesses, which is a major advantage. For example, when elbows are cut to obtain angles of less than 90°, the resulting end section remains circular, with a constant wall thickness.
For carbon steel butt-weld fittings, two standards are of worldwide importance. Compliance with both makes it possible to serve markets using imperial measurements as well as those using the metric system.
UNI EN 10253-2:2008 – Butt-welding pipe fittings – Part 2: Non-alloy and ferritic alloy steels with specific inspection requirements. This is the Italian adoption of the corresponding European standard and specifies delivery conditions for butt-weld fittings used to transport liquids and gases at both low and high temperatures.
ASME B16.9 – Factory-made wrought butt-welding fittings. This standard specifies the dimensions and tolerances for fitting manufacture, as well as marking and testing requirements. Carbon and alloy steels suitable for both high- and low-temperature service can be used.
Materials
There is a wide range of carbon steels available for the manufacture of welded fittings, depending on their intended use. Modern ISO standards mainly divide materials into two categories: steels designated according to their mechanical properties and steels designated according to their chemical composition.
Among the first group, materials carrying the suffix P are used to manufacture fittings. This designation indicates steels intended for pressure applications, generally with yield strengths starting at 235 MPa at room temperature.
The second group includes steels classified by their chemical composition, often containing significant amounts of molybdenum, which improves their strength at elevated temperatures.
For fittings intended for extremely low temperatures, non-alloy carbon steels such as P235NL or P265NL can be used. For temperatures above ambient up to particularly high operating temperatures, options include non-alloy steels such as P235GH and alloy steels containing molybdenum and other elements, such as 13CrMo4-5 or X10CrMoVNb9.
The classification under Anglo-American standards is different but conceptually similar.
Available fitting types
Reference standards leave little room for variation in fitting geometry. One major advantage is therefore having the fittings needed for plant installation readily available from stock.
The fitting types defined by the two main standards are similar and include:
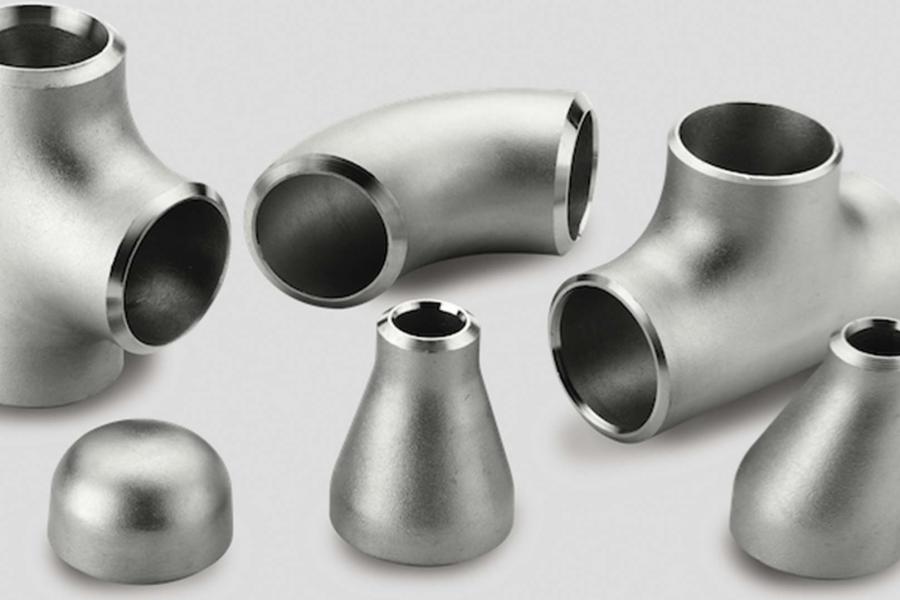
- ELBOWS: used to change the direction of fluid flow. They are available in standard and larger bend-radius versions, sometimes with a radius equal to five times the pipe diameter, reducing pressure losses where compact plant layout is not essential.
- CONCENTRIC AND ECCENTRIC REDUCERS: used to change pipe diameter along the system while minimising pressure losses.
- EQUAL AND REDUCING TEES: used to create lateral branches from the main pipeline. In specific situations, the lateral branch can be extended by welding on a short pipe section, making subsequent connection operations easier.
- DISHED ENDS: used to close off pipeline branches. Their shape helps reduce stresses at the end of the pipe by distributing them more evenly across the weld.
Why choose carbon steel as a construction material?
Carbon steel is a type of steel containing limited amounts of elements other than iron and carbon. In particular, the content of each element remains below the limits specified in BS EN 10020. Carbon therefore plays a key role in determining the material's properties.
This material is widely used in manufacturing thanks especially to its workability, which makes it suitable for many applications. Based on carbon content, it is divided into:
1. low-carbon steel (<0.3%): characterised by good weldability and softness;
2. medium-carbon steel (between 0.3% and 0.6%): commonly heat-treated by quenching and stronger than low-carbon steel. However, it is more difficult to machine, weld and cut, requiring suitable processes;
3. high-carbon steel (>0.6%): after heat treatment, it becomes extremely hard and brittle. Because it is particularly difficult to cut, form and weld, it is used in tool manufacturing.
Quality is also determined by the percentage of sulphur and phosphorus in the alloy:
- high-quality steel: when their content is <0.03%;
- superior-quality steel: when their content is <0.07%;
- ordinary-quality steel: when their content is <0.1%.
Differences between carbon steel and stainless steel fittings
Steels are high-performance materials that provide fittings with strength and durability over time, avoiding frequent replacement and the associated inconvenience and costs.
Carbon steels offer important properties for this application, but they are not the only option. Stainless steel fittings also account for part of the market. The main differences can be summarised as follows:
Chemical composition: stainless steels contain significantly higher levels of chromium and nickel than carbon steels, which consist mainly of iron and carbon with small amounts of other alloying elements;
Mechanical properties: carbon steel is generally harder and can have higher tensile strength, depending on the grade;
Cost: stainless steel is generally more expensive;
Appearance: stainless steel is often preferred, reducing the need for painting.
Both types of steel have strengths and limitations. It is therefore essential to assess plant requirements in advance and identify the main operating challenges.
Comparing carbon steel and brass alloys for fittings
The previous sections examined various aspects of carbon steel fittings, from their manufacture to their mechanical properties and strength.
However, the world of pipe fittings includes many different materials, each with its own properties and suitability for specific applications. These include brass alloys, which contain varying proportions of copper and zinc. What are the main differences between carbon steel and brass alloys?
Carbon steel is characterised primarily by excellent mechanical strength combined with hardness, making it a preferred material for applications involving significant structural loads. On the other hand, its corrosion resistance is relatively limited, which can be a drawback in particularly aggressive environments. Corrosion resistance is instead one of the advantages of brass alloys, which can be used in demanding environments even though their mechanical strength is generally lower. Another important benefit of brass is its ease of machining, which allows different shapes to be produced with less effort. Finally, appearance, while not a functional property, is also relevant: brass is often more visually appealing than ordinary carbon steel, an advantage for exposed fittings.
How can carbon steel weldability be assessed?
As discussed above, carbon steels used to manufacture fittings may have different chemical compositions, which affect the mechanical and technological properties of the components.
One widely used empirical parameter for assessing weldability is the “carbon equivalent”. It can be calculated using the following formula developed by the International Institute of Welding:
CE = C + Mn/6 + (Cr+Mo+V)/5 + (Ni+Cu)/15
where each chemical symbol represents the percentage by mass of that element in the alloy. This is one of several calculation formulas found in technical literature.
Clearly, the elements do not all carry the same weight in the formula. Some, particularly carbon and manganese, have a greater influence, while others, such as nickel and copper, have a smaller effect. It is also important to note that carbon equivalent is not the same as carbon content, which refers to the actual percentage of carbon in the alloy.
Which values are considered favourable, and which are problematic?
- CE <= 0.35: excellent weldability, with no significant difficulties;
- 0.35 <= CE <= 0.45: very good weldability, requiring few precautions;
- 0.45 <= CE <= 0.50: fair weldability, requiring particular care during welding;
- CE >= 0.50: poor weldability, making welding operations difficult.
CBAM 2026: embedded carbon in steel becomes part of import costs
On 1 January 2026, the Carbon Border Adjustment Mechanism (CBAM) entered its definitive phase. It directly affects numerous steel products, including pipe fittings classified under customs heading 7307.
The EU mechanism progressively links imports to the CO₂ emissions embedded in products, with the aim of applying a carbon cost to goods originating outside the EU that is consistent with the cost borne by European manufacturers under the EU Emissions Trading System (EU ETS).
For operators in the steel supply chain, this means that imported products are evaluated not only on raw material costs, availability and delivery times, but also on emissions generated during production.
Embedded emissions and the origin of steel
For buyers and importers of carbon steel fittings, it is becoming increasingly important to know how and where the steel was produced. Different steelmaking processes can result in very different emission levels.
CBAM rules provide for determining embedded emissions in imported goods using actual data or, where allowed by the regulations, default values. In the steel industry, the technologies used to produce steel and the entire upstream supply chain therefore become increasingly relevant.
Alongside this is the new European regime for steel imports. From 1 October 2026, for the products concerned, the “country of melt and pour” also becomes particularly important: this is the country where the steel was first produced in liquid form and subsequently cast into its first solid form.
MTCs and traceability become even more important
In this context, technical documentation plays an increasingly central role. The Mill Test Certificate (MTC), together with the heat number and other traceability records, makes it possible to link a product to its production heat and reconstruct the origin of the material.
For fittings, flanges and pipes, proper document management is therefore an integral part of supply quality. Mechanical properties, chemical composition, pressure and operating temperature are no longer the only factors: material origin, production process, embedded emissions and uninterrupted traceability throughout the supply chain are also gaining importance.
CBAM and the new European rules on steel origin are thus helping make the sector increasingly transparent, rewarding supply chains that can provide complete, verifiable and consistent technical information at every stage, from steel production to the finished component.